
Black Oxide Treatment for Joints and Bearings
Learn how chemical black oxide conversion films protect precision robotics joints and bearings against corrosion, microstructural wear, and early failure.
 October 19, 2026
 > Black Oxide Treatment for Joints and Bearings
The Failure Path That Starts at an Unprotected Surface
Corrosion in a drive train rarely arrives as a single event. A local rust spot forms first, that spot changes the dimensional relationship at the mating face, and the assembly accuracy and running smoothness of the unit change with it. As the affected area expands, friction and temperature rise together, the lubricant film breaks down ahead of schedule, and the end state is a measurable loss of positioning accuracy together with higher noise.
That sequence can run for several thousand hours before anything is recorded, and its origin is a single surface left without adequate protection. In a strain wave gear, the consequence is larger than in a conventional gearbox, because the flexspline, circular spline, and wave generator are matched to each other at tolerances measured in microns. A shift of a few microns at one interface propagates into backlash, lost motion, and torsional stiffness, which makes the dimensional relationship between the mating parts part of the product itself.
Table 1 sets out the progression and the point at which each stage becomes visible in the signals a user monitors.
| Stage | What Changes | What the User Can Observe |
|---|---|---|
| A local rust spot forms | The passive oxide layer is breached at one unprotected area | Nothing in the usual condition signals |
| The spot spreads across the fit surface | The dimensional relationship at the mating face shifts | Assembly accuracy and running smoothness degrade |
| Corrosion extends along the joint | Friction and temperature rise together | Lubricant service life shortens ahead of plan |
| Geometry and lubrication are both lost | Contact conditions move outside the design case | Positioning accuracy falls and noise increases |
Two features of that table matter for a maintenance plan. No stage is recoverable by adjustment, so once a fit surface has moved the unit has to come off the machine. Vibration and torque data miss the first three stages as well, which leaves prevention as the only intervention available in that window.
Why Hardened Steel Needs a Surface Protection Layer
Steel corrodes in humid air by an electrochemical route, and the rate rises sharply when water vapor, oxygen, and an electrolyte are present at the same time. Ions carried in cutting fluid are a common source of that electrolyte, and a machining shop supplies all three conditions at once: high air humidity, cutting fluid mist, and liquid collecting on the floor.
Precision transmission parts carry an additional problem. Hardness and wear resistance come from quenching and related heat treatment, and the martensitic structure those treatments produce is electrochemically more active than the annealed structure it replaces. Quenching that lets a tooth flank survive contact stress also makes the surface more willing to corrode, which is why surface protection on precision drive components belongs to the design case. It is also why the in-house heat treatment route and the surface route have to be planned together. A hardness specification and a corrosion specification written independently end up in conflict at the part surface.
What the Conversion Film Contributes
Black oxide treatment, also called bluing or oxidation treatment, is a chemical conversion film process. Immersion in a specifically formulated oxidizing solution grows a dense film based mainly on magnetite across the surface. It behaves differently from a coating in four ways that matter for a precision part, and Table 2 sets out each of them.
| Property of the Film | What It Means for a Precision Part | Where It Is Determined |
|---|---|---|
| Chemical conversion at the interface | The film is formed from the base metal rather than laid on top of it, so there is no bond line to peel at | Surface cleanliness of the part going into the bath |
| Micron-scale thickness | Outside dimensions and fits are unchanged, which allows the treatment on finished precision parts | Bath composition and dwell time |
| Uniform coverage on complex geometry | Deep holes and blind holes receive the same film as external surfaces | Access of the solution to the part geometry |
| Micropore structure that holds oil | A small oil reservoir forms at the surface and assists the initial running-in period | The oil dip applied after treatment |
Oil retention matters earliest in service, when the tooth flanks pass through a bedding-in phase and the reservoir supplies oil between lubrication cycles.
Where the Film Reaches Its Limits
Film performance has limits that belong in the specification as well. The film is normally paired with a subsequent oil dip or oil coating to raise rust protection further. In strongly corrosive conditions or under long-term immersion, black oxide joins a wider set of protective measures. Protection here aims at a part whose corrosion starts as late as the process allows.
Where the Treatment Is Applied in the Product Range
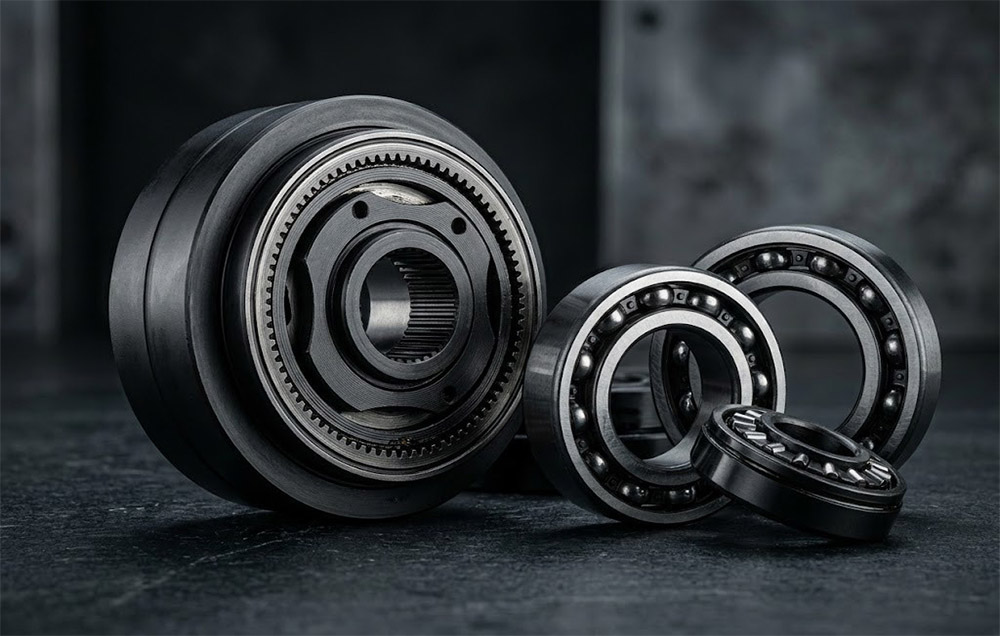
Two product families carry the treatment. First among them is the T-type joint, where black oxide raises corrosion resistance and gives an assembled robotic arm more reliable surface protection for use in humid or oily conditions. Second is a group of precision bearing products, particularly those aimed at applications with stated requirements on corrosion resistance and environmental adaptability.
Treatment coverage spans a broad specification range: the precision bearing portfolio runs from small sizes to large non-standard bearings. Small sizes test machining accuracy and manufacturing stability at small dimensions, where tolerance bands are physically short; large and non-standard bearings test structural design, process development, and production capability. Holding an equal surface quality across that range requires the same process to deliver the same film on parts whose mass and geometry differ by orders of magnitude. Learn more about our cross roller bearings.
Gear products follow the same logic. The strain wave gear series covers size 3 to size 58, reduction ratios of 30:1–160:1, and outside diameters of 13–246 mm across several hundred SKUs. The hat type FHT configures the same gear set for a different mounting interface. Every part in that range has to carry its own surface treatment specification.
Coordination with Sealing, Material and Lubrication
Treatment is one element of a protection system, and it fails when the elements around it are specified separately.
The Sealing Interface and the IP67 Rating
Sealing is the clearest case. A joint module assembly carries an IP67 ingress protection rating, and that rating belongs to the assembled unit, where the seals, the seal grooves, and the surface finish act as one barrier. A film that changes the surface roughness inside a seal groove changes the contact and the leakage path of the seal running in it.
Lubrication and Grease Compatibility
Lubrication raises a similar interface. Grease has to remain in the flexspline cavity for the whole service interval without attacking either the elastomer or the film. The sealing mechanism is specified per FHT-I, FHT-II, and FHT-V with defined oil seal and groove dimensions. Assembly requirements cover the seal at the input fixed end against the circular spline and flexspline, the seal at the output end against the circular spline, and the grease fill in the flexspline cavity. A surface film that retains oil in its micropores draws its oil supply from the same grease.
Material State and Surface Preparation
Material state reaches back to the previous section. Film quality depends on the roughness and cleanliness of the incoming part, which are set by heat treatment and by precision machining. A film grown on a surface carrying residual scale or embedded contamination will not match one grown on a properly prepared surface, whatever the bath parameters are.
| Parameter | Specification | Note |
|---|---|---|
| Joint module ingress protection | IP67 | Belongs to the assembled unit, where seals and surface finish act together |
| Joint module outside diameter | 40 mm to 190 mm in continuous steps | Spans the equivalent of size 8 to size 40 |
| Surface treatment on T-type joints | Black oxide | Specified for humid or oily service conditions |
| Positioning accuracy | ±15 arcseconds | Output side |
| Design life | 10,000–15,000 hours | At the stated load and speed |
| Backlash by series | ≤60, ≤30, and ≤20 arcseconds | Population value per series |
| Rated torque | Permissible continuous load torque at a rated input speed of 2,000 rpm | Catalog definition |
| Precision bearing range | Small sizes to large non-standard sizes | Surface quality held across the full range |
Why the Process Is Held In House
Surface treatment is a critical process, and keeping it inside the same system as the operations around it allows the process parameters to be tuned as one set. Quality of the film tracks the surface state produced by heat treatment and precision machining, and when all three sit in one organization, the parameters can be adjusted against each other. Spread across separate suppliers, each operation can only run inside its own capability limit.
Laifual Drive runs heat treatment, precision machining, and gear cutting as in-house operations, and it has built its own special steel melting and flexspline precision forging lines. The full process chain is described under Laifual Drive precision manufacturing. Gear cutting uses a self-developed process, with core component machining time reduced from two to three hours to less than 15 minutes. The tooth form that results depends on the same surface condition the treatment stage works from, as covered in precision gear shaping technology. Surface treatment shares one quality system with the stages on both sides of it.
This argument concerns maintenance cost. When the protection layer and the surface it grows on come from one process system, the corrosion rate a user experiences is a controlled output instead of a variable inherited from several suppliers. Over a design life of 10,000–15,000 hours, the difference shows up in how often a unit has to come off the machine. That interval is normally the dominant term in the cost of ownership of a joint.
Specifying Surface Protection
Surface treatment changes none of the core parameters of a drive, and it changes service behavior directly. For equipment that runs in a workshop, at a wash station, or in a semi-outdoor location, it is the hidden variable that sets the maintenance interval. That point in the failure path is where the least expensive intervention is still available.
For a design engineer, the practical consequence is that surface protection belongs in the specification with the same status as the load case. State the duty environment, the humidity and fluid exposure, and the expected maintenance interval alongside the load case. Then confirm that the assembly ingress protection level, the surface treatment, and the grease specification are consistent with each other. That review takes minutes at the drawing stage and replaces a field failure that produces no diagnostic signal for thousands of hours.
Need Customized Environmental Protection?
Our tribology engineers provide chemical compatibility reports, specialized sealing configurations, and accelerated salt-spray validation for severe duty cycles.